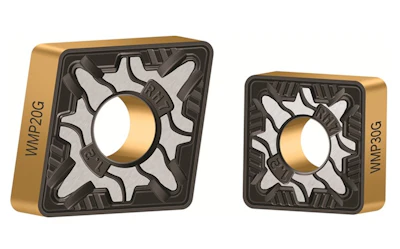
Walter (Greer, SC) presents the RM7 roughing geometry to maximize stability when turning challenging stainless steel workpieces. The cutting edge design prevents fractures caused by chip impact. The geometry is available in five basic forms: CNMG, DNMG, SNMG, TNMG and WNMG.
The RM7 negative basic shape geometry is an alternative to the RM5 geometry if it is prone to fractures. In addition, the new RM7 geometry can be run at a higher axial depth of cut and feed rate than the RM5, as well as the MM5 and FM5 geometries.
Applications include roughing against the shoulder, interrupted cuts and turning components that are out of round or difficult to machine, such as one with a weld seam. The RM7 geometry is suitable when the strength of the MM5 or RM5 is not sufficient. Additionally:
- Strength is maximized with a cutting edge that features 0.10 in × 6° protective chamfer and a 20° positive rake angle. This is the ideal combination for stability and soft cutting in stainless steel.
- An enlarged contact surface enhances stability, and a coolant jet guide improves cooling.
- The strong cutting edge of the RM7 geometry for rough turning leads to reliable high volume production and reduced downtime.